MIM for small, complex precision parts in series production
Metal Injection Molding (MIM) is suitable for the production of small, highly detailed precision parts in series. Depending on the part design, cutouts, threads, engravings, and fine contours can be incorporated directly into the mold. Richter Formteile assesses suitability based on your requirements, advises you on materials and production-friendly design, and supports your project through to the agreed-upon delivery condition.
What is Metal Injection Molding?
Metal Injection Molding, or MIM for short, is a manufacturing process for complex metal parts. In German, it is referred to as “metallpulver-spritzguss” (metal powder injection molding). In this process, fine metal powder is mixed with a binder to form an injection-moldable raw material, known as feedstock. This material is molded in a die, then debound and sintered. During sintering, the component compacts and shrinks in a controlled manner to its intended final dimensions. This shrinkage is already factored into the die design. This allows for the production of geometries that would be achievable only with greater effort using conventional powder compaction or purely machining processes. MIM particularly demonstrates its strengths with small precision parts, where holes, threads, engravings, or other details can be incorporated during the shaping process. Richter Formteile evaluates whether these possibilities can be utilized technically and economically for your precision part based on component size, geometry, material, quantity, and tolerances. On this basis, we advise you on a production-ready design and coordinate implementation with a suitable production partner.
On this page
When is MIM suitable for a component?
Several of the following characteristics suggest that MIM should be examined more closely. The final suitability depends on the drawing and the requirements for the finished part.
A lot of detail in a small space
Holes, threads, engravings, and fine contours can be incorporated during the molding process. Which details can actually be implemented depends on the mold design, demolding, wall thicknesses, and material.
Recurring Series Demand
MIM requires a mold. The cost of producing the mold must be commensurate with the planned demand. The process is therefore particularly attractive when complex parts are manufactured repeatedly in sufficient quantities.
Fewer individual parts and assembly steps
MIM can combine features in a precision part that would otherwise require multiple individual parts, assembly steps, or machining operations. Whether these steps can actually be reduced is determined based on the specific design.
Metallic properties and a specific material
MIM processes metal powders based on a specified alloy. The material, heat treatment, and delivery condition are tailored to the component's requirements.
Design for Manufacturing
Consistent wall thicknesses and appropriate transitions promote controlled demolding and sintering shrinkage. Early coordination helps prevent warping, material buildup, or unnecessarily tight tolerances.
One of several methods
MIM is not the best solution for every component. For components of different sizes, under different loads, made of different materials, or in mass-production settings, investment casting, conventional sintering, die forging, or machining may be more suitable.
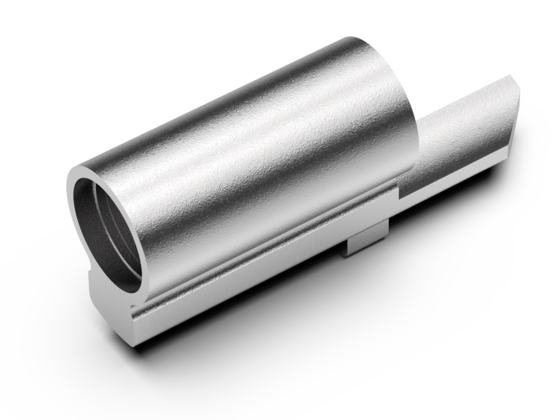
Can your component be manufactured using MIM?
Please send us your drawing and any project details you already have. To help us assess your needs initially, please provide information on the material, planned requirements, tolerances, operating conditions, and desired delivery condition. If not all details have been finalized yet, we will work with you to determine what information is needed for further review.
Comparing MIM with Other Processes
How does the MIM process work?
Your drawing and the requirements for the finished component determine how we set up your MIM project. Richter Formteile works with you to determine the material, functional dimensions, and delivery condition. We coordinate tooling, manufacturing, and testing with the selected production partner and oversee the implementation through to series production approval.

1. Mix
In the first step of MIM technology, the fine metal powder is kneaded and heated according to its desired alloy with thermoplastic material as a binder to form a homogeneous powder mixture.

2. Feedstock
After granulation, the metal mixture – the feedstock – is viscous and can now be processed in the injection molding process.

3. Injection molding
At elevated temperature, the feedstock is now injected into a closed mold at high pressure. The form is first filled in completely and then plasticized.
The resulting green body has all the geometric properties of the finished component.

4. Debinding
The cooled green body is now removed from the injection molding machine. The binder is removed in a two-stage process, thermal or catalytic debinding. This can take up to 24 hours.
What remains is a purely metallic, but still open-pore component, the so-called brown body.

5. Sintering
n order to make a precision molded part with the desired geometric and mechanical properties out of the brown body, it has to be sintered at high temperatures.
The molded part can then be treated further if necessary.

6. Final inspection
All our parts are subjected to a comprehensive visual inspection after the MIM process has been completed.
The entire scope of all criteria and measures of quality control is coordinated in a functional manner depending on customer requirements.
The MIM Process in a Video
Designing for MIM
The quality of a MIM component isn’t determined solely during the manufacturing process. It begins with a design that takes into account shaping, debinding, and sintering shrinkage. That’s why we coordinate wall thicknesses, tolerances, and critical geometries with you and our production partner early on.

Design wall thicknesses to be as uniform as possible
Significant variations in wall thickness can lead to uneven cooling, binder removal, and shrinkage. Appropriate transitions and material distribution that is as uniform as possible help ensure a stable process.
Account for shrinkage in the mold
The green part is formed larger than the finished component. During sintering, the microstructure densifies and the part shrinks. This oversize is tailored to the material, geometry, and process. Therefore, the mold dimensions cannot be derived universally from a single general shrinkage value.

Coordinate Details with the Tooling Concept
Depending on the geometry, holes, contours, threads, engravings, or undercuts can be incorporated as early as the shaping stage. The key factors are whether they can be reliably filled, demolded, supported during sintering, and machined to the required tolerance.
Specify tolerances where they are needed
Not every dimension requires the same level of accuracy. If function-critical dimensions are specified early on, the tool, process, and any necessary post-processing can be specifically designed to meet those requirements.
Key MIM Terminology
You Should Know These Terms
An injection-moldable material consisting of metal powder and a binder system. It is typically processed as granules in an injection molding machine.
Organic components that hold the metal powder together for shaping and make it flowable. The binder is largely removed before and during sintering.
The molded part immediately after injection molding. It still contains the binder, has not yet reached its final dimensions, and is more mechanically fragile than the finished part.
The porous component after a significant portion of the binder has been removed. It is then sintered and compacted during this process.
A thermal process conducted below the melting temperature of the base material. The metal particles bond together, the component is compacted, and it shrinks to its intended final dimensions.
The ratio of the achieved component density to the theoretical density of the material. The specific value depends on the material and the process.
Debinding refers to a two-step process used in the production of castings via the MIM process. In this process, thermal or catalytic debinding is used to remove the binder from the green compact, leaving a purely metallic component.
Advantages and Limitations of MIM
MIM allows for a high level of geometric detail in small, precision parts and can therefore reduce the number of individual parts or eliminate additional machining steps. At the same time, the process imposes specific requirements on part size, design, tooling, and production volume.
Holes, threads, engravings, and fine contours can be incorporated during the shaping process
Tooling and start-up costs must be in line with the planned production run
The features of several individual parts can be combined into a single precision part
Part size and wall thickness affect demolding, process duration, and cost-effectiveness
High level of detail in small precision parts and appropriate component design
Shrinkage and possible warping must be taken into account in the design
Reproducible mass production following successful process design
Tight tolerances depend on the specific dimension, material, component, and condition upon delivery
Different metallic materials and property profiles
Further processing may still be necessary
Potential to reduce machining and joining steps
Not every geometry, quantity, or material requirement can be effectively met using MIM.
When MIM Isn't the Best Solution
A complex metal component does not necessarily have to be produced using the MIM process. Depending on the size, load, material, quantity, and desired delivery condition, investment casting, conventional sintering, or die forging may be more suitable. Richter Formteile therefore does not limit itself to a single process. We compare the requirements of your component with the capabilities of our four manufacturing processes and identify which solution makes the most sense from both a technical and economic standpoint.
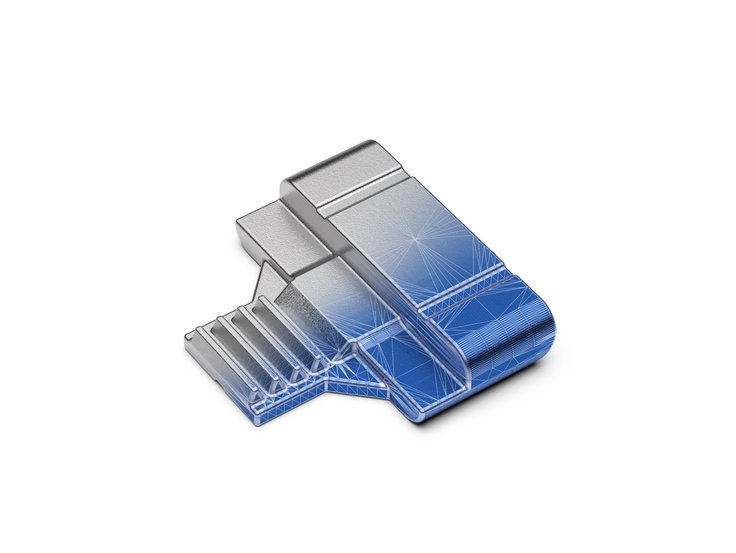
Precision Casting
Investment casting for custom precision parts—featuring intricate contours and internal geometries made from a wide range of castable alloys.
View Investment Casting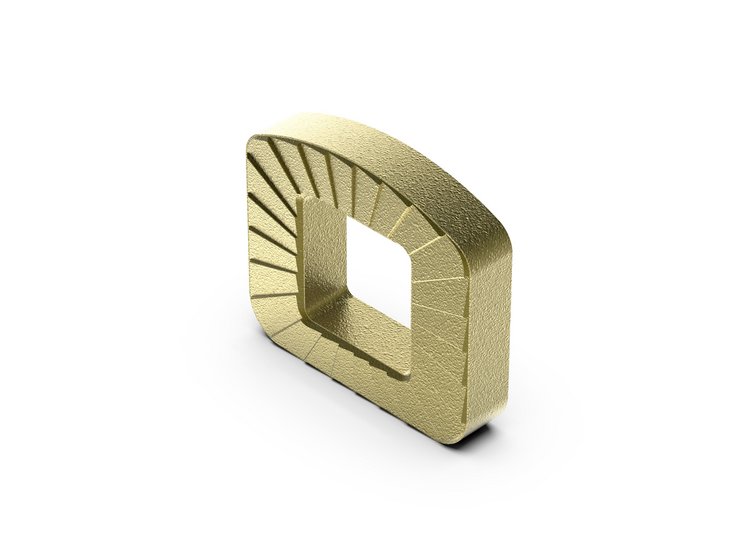
Sintering
Pressing and sintering for mass-produced components—with many contours already formed in the die, eliminating the need for time-consuming milling or turning.
View Sintering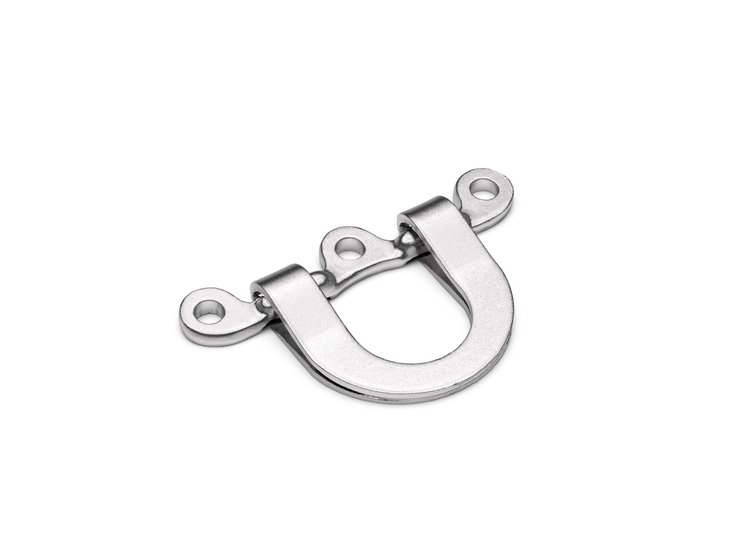
Die forging
Forged components for high loads—with materials and designs tailored to the forces your component must withstand during operation.
View Die ForgingMIM Materials at Richter Formteile
The choice of material determines the mechanical, thermal, or corrosion-related properties that a MIM component can achieve. Therefore, it is not only crucial whether a material can, in principle, be processed using the MIM process. It must also be available for the specific geometry, production process, and desired delivery condition. Richter Formteile provides technical data sheets for various MIM material groups. Together, we determine which material is best suited to the component’s function, operating conditions, heat treatment, and further processing steps.
In which industries is MIM used?
MIM is used in various industries when small, precision parts need to combine many details in a confined space with a recurring production demand.
Mechanical Engineering
Complex functional parts, levers, housings, and components with defined functional surfaces
Vehicle Manufacturing
High-performance components with complex geometries and reproducible mass-production characteristics
Drive Technology
Geometrically complex components for power transmission and motion functions
Fittings and Pumps
Components in contact with media or subject to pressure, selected based on material and testing requirements
Electrical Industry
Metallic functional and housing components with complex contours
Medical Technology
Small and complex components with high requirements for materials, surface finishes, and testing
Technical MIM Data at Richter Formteile
The achievable values depend on the component size, geometry, material, process, and agreed-upon delivery condition.
standard weight:
0.001 - 0.150 kg
production:
Asia
certified acc. to:
DIN ISO 9001, 14001, IATF 16949
tolerances:
approx. +/- 0.3% of the nominal size
surfaces:
Ra 3.2
materials:
steel, stainless steel, hard metal and copper
post-processing:
own CNC processing centers, heat treatments according to customer specifications
Your MIM Project with Richter Formteile
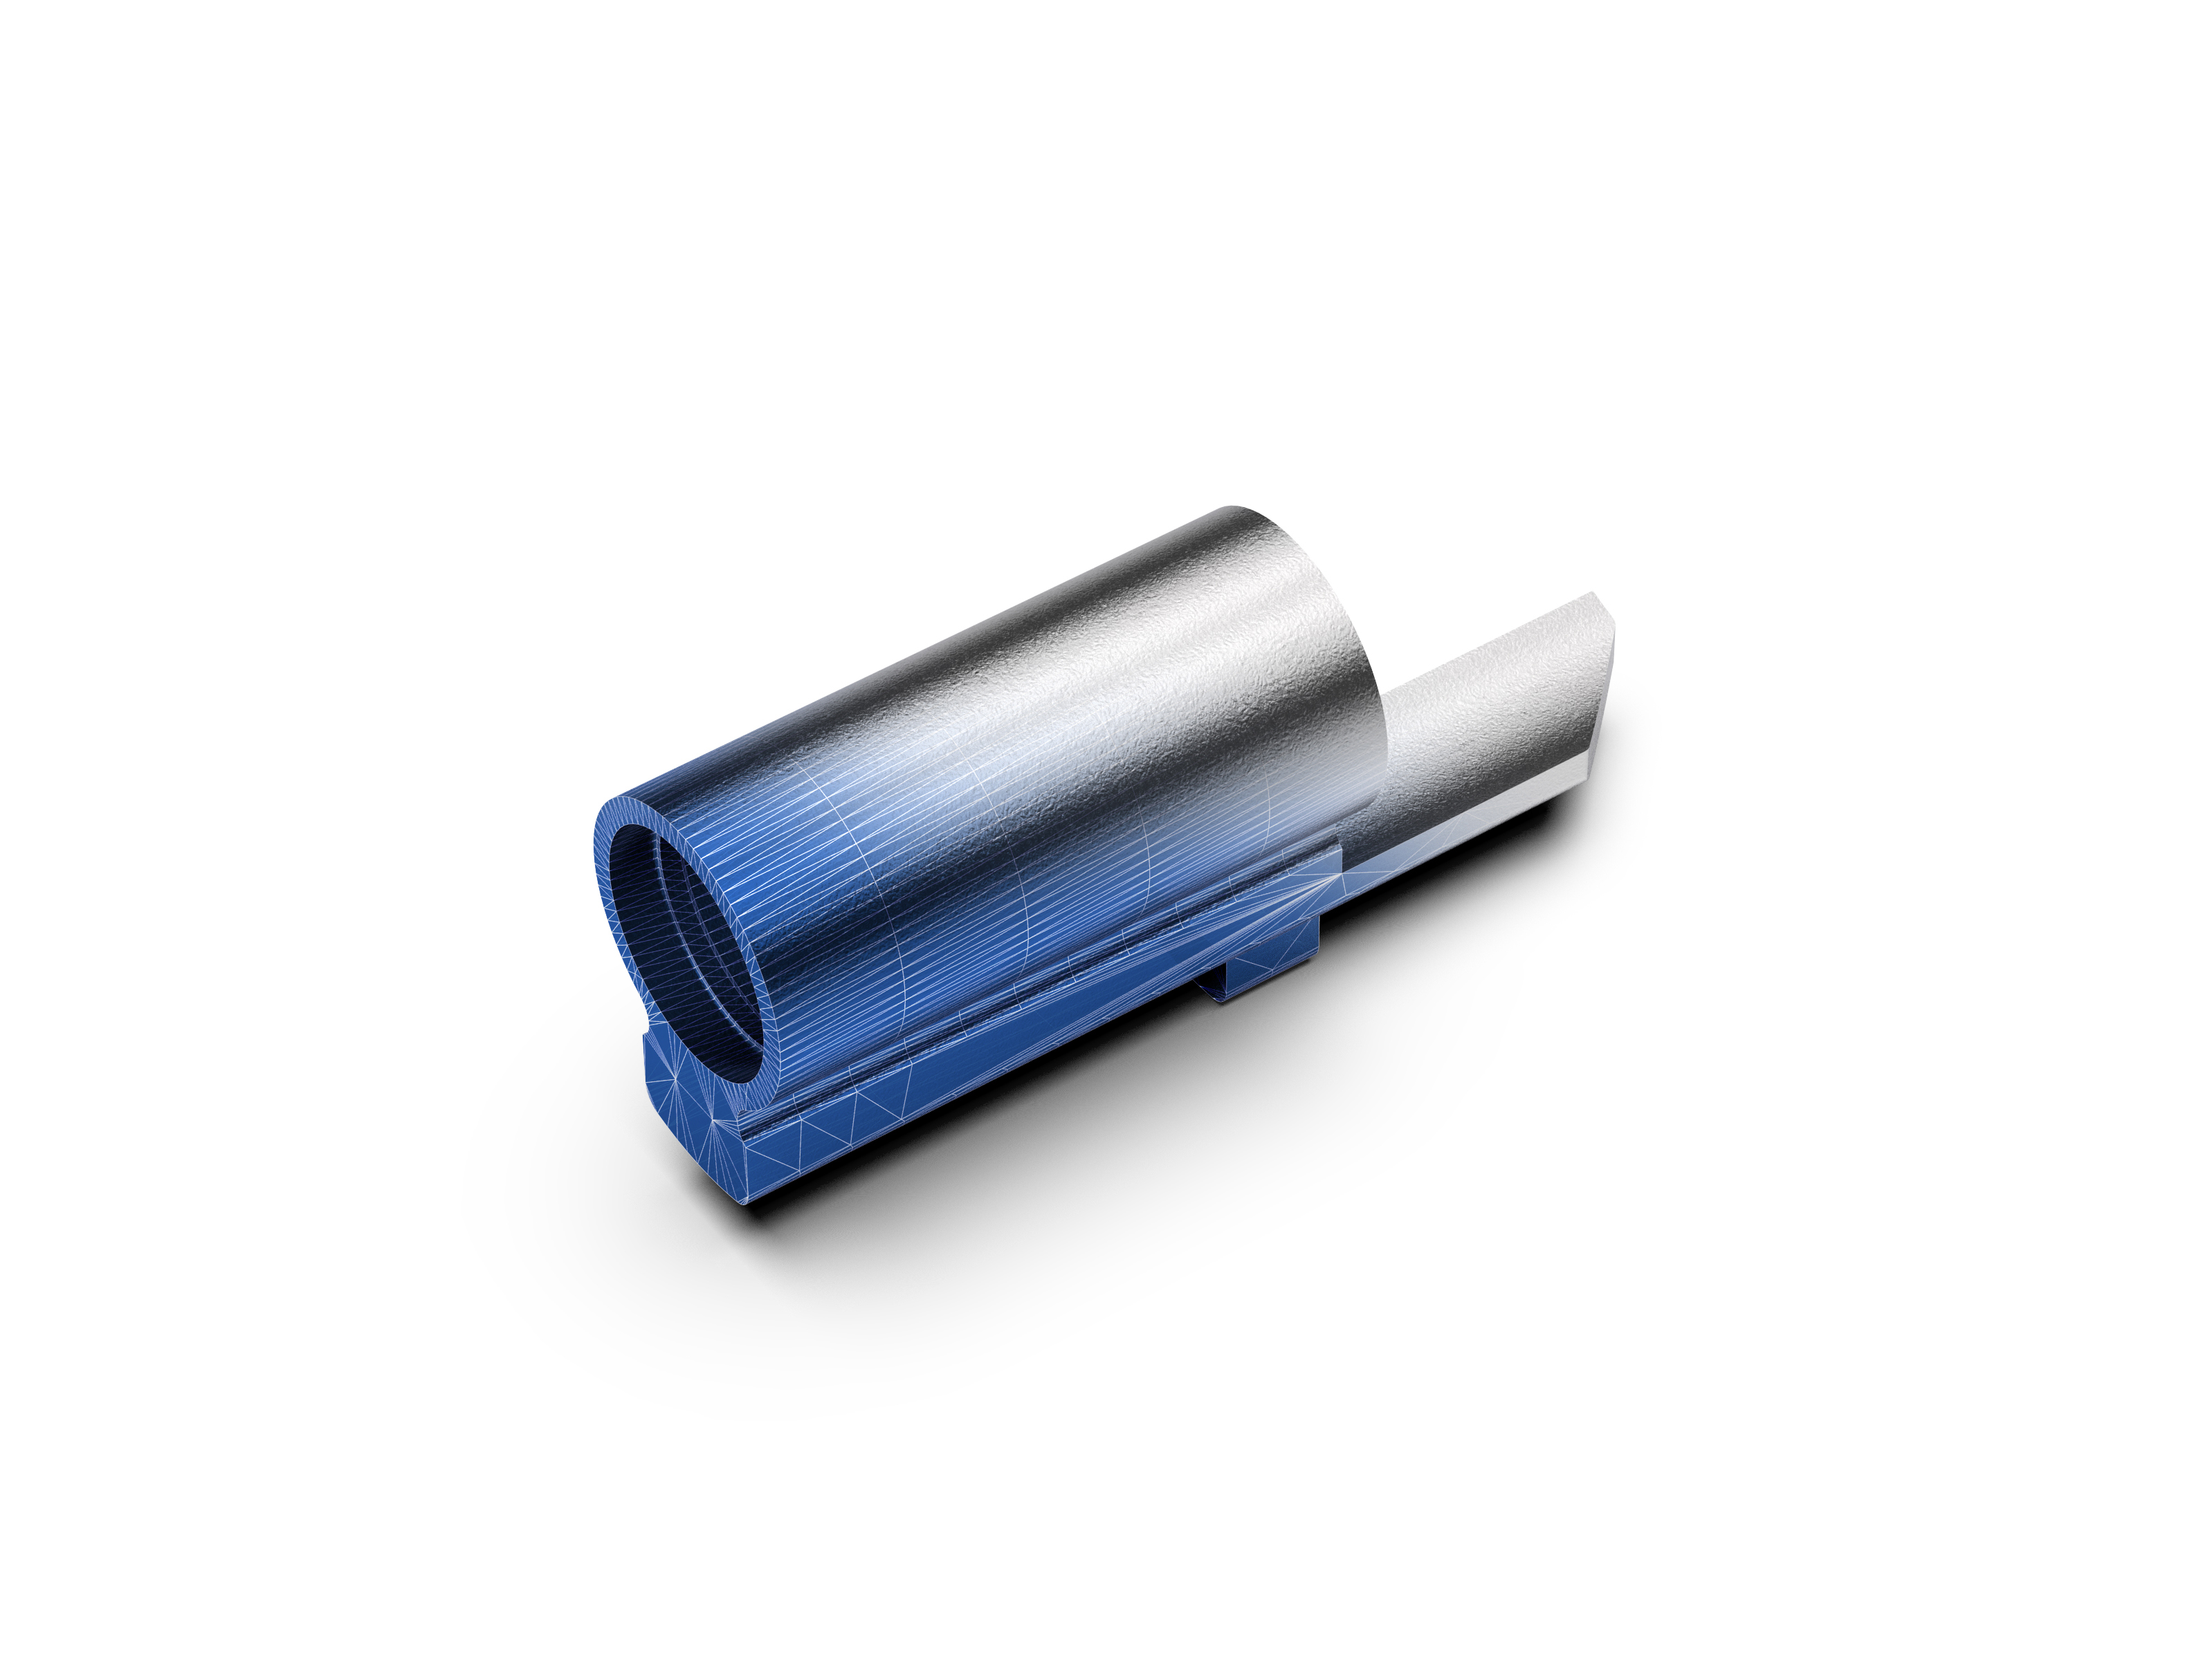
You provide us with your drawing and tell us what the component needs to be capable of. We review the technical feasibility and select a suitable manufacturing partner from our international network.
Richter Formteile coordinates tooling and prototyping. Series production begins only after you give your approval.
If necessary, we coordinate mechanical machining, heat treatment, surface treatment, or assembly.
Full Service for Your MIM Component
In addition to technical project support, Richter Formteile offers further advantages that ensure reliable project execution and supply:
- Contract Partner in Germany
: Richter Formteile coordinates the production partners involved and remains your designated point of contact. - On-site
Quality Inspection: The agreed-upon processes and quality characteristics are inspected directly at the production partners’ facilities. - Pre-financing and warehousing
Richter Formteile pre-finances and produces the agreed-upon quantities within the agreed-upon framework and stores them in Leonberg. - Just-in-time delivery upon request
The agreed-upon batch sizes are delivered from the warehouse in Leonberg as needed.
Let's talk about your MIM component
Frequently Asked Questions
About MIM and MIM Projects
In metal injection molding, metal powder is processed with a binder to form an injection-moldable feedstock. This feedstock is molded in the die, debound, and then sintered. During this process, the component is compacted and shrinks in a controlled manner to its intended final dimensions.
MIM is particularly well-suited for small metal components with complex geometries and recurring production needs. Whether the process is technically and economically feasible depends, among other things, on the component size, material, tolerances, tooling costs, and planned production volume.
Achievable tolerances depend on the specific dimension, geometry, material, component size, and desired delivery condition. Dimensions relevant to function are therefore checked for the specific component. If necessary, additional machining steps can be coordinated.
Richter Formteile offers a variety of steel and other metallic materials for MIM projects. The company determines which materials are currently available and suitable for a given application based on the component requirements and technical data sheets.
Depending on the component and the agreed-upon delivery condition, Richter Formteile coordinates mechanical machining, heat treatment, surface treatment, or assembly. The specific scope of services is defined in the project.
Initial technical coordination can begin based on the component's function, installation situation, planned quantity, and known requirements. To conduct a reliable feasibility study and evaluate a quote, a drawing or appropriate 3D data will be needed later in the process.
Richter Formteile remains your point of contact for technical clarification, production partnerships, quality, and delivery. The exact terms of the contract and the services involved will be specified in the quote.
Your Contact for MIM
Would you like to discuss a geometry, a material, or the appropriate manufacturing process? Your contact person will work with you to determine what information is needed for an initial technical assessment.
Timo Richter
Managing Director
+49 7152 90171-0
t.richter@richterformteile.com
Let's talk about your MIM component
Please send us your drawing or the project details you already have. If any information is missing, we will work with you to determine what else is needed for the technical review.