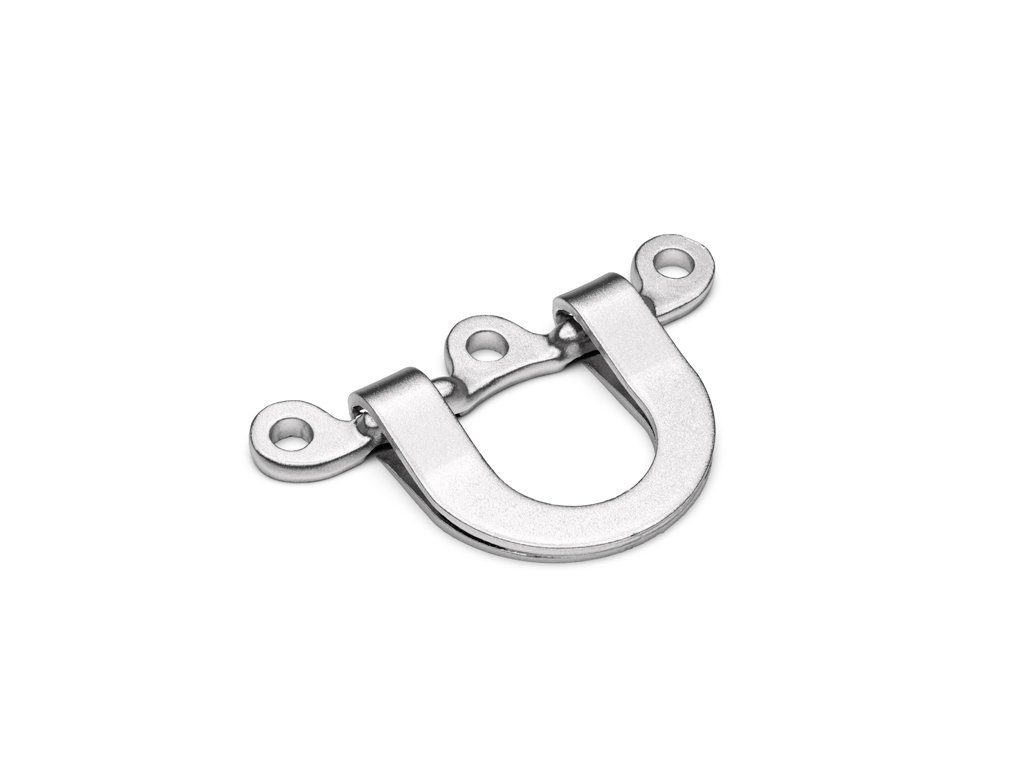
Forged components for high loads
In die forging, metal is shaped into components that must transmit forces and withstand recurring loads. Richter Formteile advises you on material selection and production-oriented design, selects the appropriate production partner, and manages your project from tooling and prototyping through to series production. Based on your drawings, we work with you to determine which surfaces require finishing and which properties must be verified.
What is die forging?
Die forging is a solid-state forming process. In this process, solid metal is shaped by pressure or impact between shaping tools. These tools are called dies. Their inner contour determines the shape into which the material flows. Depending on the material and the manufacturing task, forming is performed hot, semi-hot, or cold. Among other factors, the temperature influences the forming forces required and the properties that can be achieved. The manufacturing process shown on this page illustrates hot forming, in which the raw material is heated before forging.
On this page
When is die forging the right choice for your component?
High mechanical stress may make die forging a suitable option. However, whether this process is right for your component depends on the overall manufacturing task. To determine this, Richter Formteile reviews your drawing, the operating conditions, and your planned requirements, along with any necessary follow-up work.
Stress
Does the component transmit forces, is it subjected to alternating loads, or does it need to absorb impacts? These requirements form the basis for material selection and design. We’ll discuss areas subject to particularly high stress with you early on.
Geometry
The contour must be formed within the mold and then be able to be removed. We work with our production partner to determine how the material will be distributed and which features should be created through additional machining.
Material
Strength alone rarely fully describes the application. Toughness, wear, corrosion, and operating temperature can also be critical factors. These requirements determine the appropriate alloy and the required material condition.
Functional Dimensions
Fits, sealing surfaces, and threads have different requirements than the forged outer contour. We determine which features must already be present on the blank and which will be machined afterward.
Production requirements
Tooling and production ramp-up involve costs that must be commensurate with demand. To assess the economic viability, we also consider material usage, post-processing, and inspection. These factors determine whether die forging is economically viable for your production run.
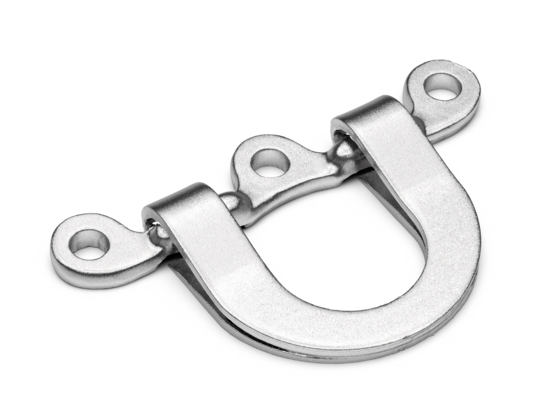
Is drop forging suitable for your component?
Send us your drawing or existing 3D data, along with details on the application and your projected annual demand. Richter Formteile will work with you to determine whether die forging is suitable for the task and identify any material or manufacturing issues that still need to be clarified.
Comparing Die Forging with Other Processes
How are drop-forged parts made?
Richter Formteile works with its production partner to translate your requirements into a manufacturing plan: Which material will be used, how will the contour be formed, and what machining and inspection steps will follow? The seven steps outline the typical process for hot die forging. Individual operations and their exact sequence depend on the material and the component; interim inspections may also be scheduled.
1. Warming
The first step consists of separating the blank from the semi-finished product, which is brought to the required temperature for forming in the furnace.
Various systems are used for heating, which heat the workpiece in such a way that the temperature is above the austenitization temperature of the respective material. The following systems are used: inductive heating systems, conductive heating systems, natural gas-powered chamber furnaces.

2. Forging process
First, the blank is separated from the semi-finished product and brought to the workpiece temperature.
With the help of rollers, presses or an air hammer, the heated blank is preformed if necessary.
3. Forging process
In the next step of the forging process, the blank is placed in a closed die.
The upper and lower dies contain the contour of the desired forging as a negative and press the blank into the appropriate shape with several strokes.
Excess material is pushed into the ridge.
4. Deburring
During this step, the protruding burr is removed (deburring). Specific deburring tools are used for this. If necessary, this work step can be supplemented by punching the workpiece.
After the forging has been completed, it is possible to reshape it using the die.

5. Tempering of drop forgings
This is followed by the final tempering (heat treatment) of the forgings in furnaces.
6. Descaling
The scale layer created is now mechanically removed from the forging.

7. Final inspection
After the forging process has been completed, all precision molded parts in metal forming technology are subjected to a comprehensive visual inspection.
The entire scope of all criteria and measures of quality control is coordinated in a functional manner depending on customer requirements.
Die Forging in a Video
Designing Components for Die Forging
The parting line determines where the two halves of the mold meet. Together with appropriate draft angles, it influences how easily the part can be removed from the mold. Transverse features and undercuts may require additional machining or special mold designs.
Radii and appropriate cross-sectional transitions facilitate material flow. Sharp changes in cross-section and areas that are difficult to fill must be taken into account during mold design. The component’s function and the stresses it will be subjected to remain the decisive factors.
Whenever fits, threads, or particularly precise mating surfaces are required, we factor in the subsequent machining in our design. The allowances must provide sufficient material for this purpose. At the same time, the forged contour should minimize unnecessary machining effort.
With a flash:
Some of the material flows into the narrow space between the die halves. The flow resistance created there helps fill the mold contour. The resulting flash is then removed. Material usage and deburring are therefore part of the production planning.
Without a flash:
The blank’s volume must match the mold contour with exceptional precision. The mold and process are closely coordinated accordingly. The potential material savings must be weighed against the requirements for the blank and the process. Richter Formteile works with its production partner to determine which method can economically produce your contour and the required dimensions.
How does the fiber orientation affect the load-bearing capacity?
During forging, the material flows as it is shaped. In the process, microstructural components and inclusions align themselves along this flow. This internal structure is referred to as the grain orientation. It can cause the material to behave differently under stress in different directions.
A fiber orientation that matches the applied load can enhance the load-bearing capacity of a forged part. This is particularly relevant for components that transmit forces or are subjected to repeated load cycles. The key factors are how the load acts on the component and whether the design takes this direction into account.

Richter Formteile therefore works with you to identify where forces act and which areas are subject to particular stress. This information supplements the drawing and is incorporated into the coordination process with the production partner. In addition to the fiber orientation, the alloy, heat treatment, geometry, and subsequent machining also determine the material’s properties. The required load-bearing capacity and the method for verifying it are specified for each individual component.
Advantages and Limitations of Die Forging
Arguments in Favor of the Procedure
- The material and forming process can be tailored to components subjected to mechanical stress.
- A fiber orientation designed to withstand the expected stresses can enhance the component’s load-bearing capacity.
- Forming tools enable the repeatable production of a component contour in series.
- The forged blank can reduce the amount of subsequent machining compared to manufacturing from solid material.
What Goes Into the Decision
- Tooling and production ramp-up must be aligned with planned demand.
- Material flow and demolding limit the geometry that can be forged directly.
- Burrs, machining allowances, and follow-up operations affect material usage and costs.
- Tight functional dimensions and specific verification requirements may necessitate additional machining and inspections.
When selecting a process, Richter Formteile considers these factors together with the required delivery condition. The determining factor is the cost of the finished component.
Which process is right for your drawing?
For complex casting geometries, investment casting may be an alternative. MIM is particularly suitable for small, complex metal parts produced in series. Conventional pressing and sintering are suitable for geometries that can be formed and removed within the pressing die. Richter Formteile compares the manufacturing processes based on your drawing, the required properties, and the effort involved in producing the finished component.
Precision Casting
Investment casting for custom precision parts—with intricate contours and internal geometries made from a wide range of castable alloys.
View Investment Casting
MIM
Metal injection molding for small, highly detailed precision parts in series production—with threads, engravings, and fine contours already incorporated into the mold.
View MIM
Sintering
Pressing and sintering for mass-produced components—with many contours already formed in the die, eliminating the need for time-consuming milling or turning.
View SinteringForging Materials at Richter Formteile
At Richter Formteile, steel, stainless steel, and aluminum are suitable materials for drop-forged parts. The specific choice of material depends on the intended application of your component. We coordinate the required properties and delivery condition with you and determine the appropriate alloy with our production partner.
Steel
For components that transmit forces or absorb alternating loads, strength and toughness are the top priorities. The steel grade and material condition are tailored to these requirements.
Stainless Steel
When corrosion resistance or specific operating conditions are critical, stainless steel may be the right choice. The appropriate grade depends, among other factors, on the medium, temperature, and mechanical stress.
Aluminum
Aluminum is a viable option when low mass is important for the component’s function. The alloy, geometry, and material condition must ensure that the required mechanical properties are met.
Do you already have a material specification? We’ll incorporate it into our technical evaluation. We’ll coordinate other alloys and their availability specifically for your project.
Where are drop-forged parts used?
Drop-forged parts are found, among other places, in drive systems, load-bearing joints, and tools. The following examples illustrate typical component applications. Whether drop forging is suitable for your application depends on your specific requirement
Power transmission, such as connecting rods or shafts
Load cycles, strength, and precise bearing and mating surfaces
Load-bearing or connecting components, such as chassis components
Loads, Geometry, and Application-Specific Verifications
Tools, such as wrenches
Load-bearing capacity, wear behavior, and suitable material condition
Technical Specifications for Forged Parts from Richter Formteile
The achievable values depend on the component size, geometry, material, process, and agreed-upon delivery condition.
standard weight:
0.04 - 150 kg
production:
Europe, Asia
certified acc. to:
DIN ISO 9001, 14001, IATF 16949
materials:
steel, stainless steel alloys and aluminum
post-processing:
own CNC processing centers, heat treatments according to customer specifications
approvals in the fittings area:
AD 2000 and TRD 100
What dimensions and properties does your component require?
The requirements for a forged blank differ from those for a fully machined component. Richter Formteile works with you to determine the condition in which the features must be present—this clarifies what is formed in the die and what comes next.
Dimensions and Geometry
External contours, cross-sections, and component dimensions as the basis for tooling and manufacturing
Dimensional Specifications and Tolerances
Reference surfaces, required accuracy, and machining condition of the individual features
Surface
Requirements for Forged, Cleaned, Machined, or Treated Surfaces
Material Condition
Alloy and required properties following the intended treatment
Condition upon delivery
Scope of Machining, Surface Treatment, Inspection, and Documentation
Achievable tolerances depend, among other things, on the material, component size, geometry, and manufacturing process. Additional machining may be necessary for tight fits or specific surface requirements. This is taken into account during the design of the raw part.
From the forged blank to the agreed-upon delivery condition
Finish editing the functional areas
Holes, threads, fits, or mounting surfaces can be created through machining after forging. In addition, depending on the material and application, appropriate heat treatments and surface treatments are performed. Richter Formteile coordinates the agreed-upon follow-up work with the production partner and the machinists involved. In doing so, we specify which machinist produces the respective functional dimensions and surfaces and in what condition the component is handed over.
Demonstrate the required qualities
Dimensional inspection, surface inspection, and material testing address different issues. In addition to geometric characteristics, properties such as strength, hardness, or toughness may need to be verified. If the application requires it, appropriate non-destructive testing methods are also used. The appropriate method depends on the material, geometry, and the type of defect being sought. We will coordinate with you to determine which features will be inspected, the scope of the inspection, and what documentation you require. These agreements form the basis for sample testing and production inspection. Richter Formteile will resolve any deviations with the production partner.
Your Forging Project with Richter Formteile
At Richter Formteile, your drawings, quality requirements, and delivery agreements all come together. We manage the collaboration with our manufacturing partner and remain your point of contact for technical questions, changes, and delivery.
-
Clarify Requirements
We will discuss your drawing, the application, the material, and your projected needs. Based on this information, we will select a suitable manufacturing partner and coordinate the technical implementation. The quote will detail the services for tooling, prototyping, manufacturing, and follow-up work.
-
Prepare the tooling and initial prototypes
Once you place your order, we will coordinate tooling and prototyping. Our manufacturing partner will produce the initial prototypes. The agreed-upon characteristics will be tested and documented. You will receive the prototypes and the initial prototype test report for review at your facility.
-
Share the series
We will discuss any deviations and necessary changes with you and the production partner. Series production will not begin until you have approved the initial samples. During production, Richter employees inspect the molded parts, and independent inspectors verify the agreed-upon processes and quality characteristics at the production partner’s site.
-
Arrange for delivery
We coordinate production up to the agreed-upon delivery stage and arrange for transportation as well as import and customs clearance, if necessary. We coordinate quantities, deadlines, and call-offs with your demand planning.
-
Full Service for Your Forged Part
Richter Formteile manufactures and finances the agreed-upon quantities within the agreed-upon framework. We store the inspected components in Leonberg. You call off the agreed-upon lot sizes as needed and pay for the quantity delivered each time. Richter Formteile in Germany remains your contractual partner.
Frequently Asked Questions
About Drop Forging and Your Project
In die forging, contoured dies determine the shape of the component. In open-die forging, the shape is created through forming with simple tools and the controlled guidance of the workpiece. The appropriate method depends, among other things, on the geometry, dimensions, and requirements. For die-forged parts, the cost of the shaping die must be taken into account when selecting the process.
No, a general ranking cannot be derived from this. The material, geometry, heat treatment, and load conditions determine the component’s load-bearing capacity. A properly designed fiber orientation can be an advantage of forging. Richter Formteile therefore considers the requirements for your specific component and the necessary validation before classifying a process.
In flash forging, material flows into the flash area between the die halves. This aids in filling the mold; the flash is subsequently removed. Flashless forging requires particularly precise coordination of the blank volume, die, and process. We will work with our production partner to determine which method is appropriate and available for your component.
This depends on the material, geometry, component size, and manufacturing process. Another key factor is whether a dimension is required on the forged blank or after additional machining. Tight functional dimensions may require machining. Richter Formteile will work with you to determine which features must be maintained and inspected in which condition.
At Richter Formteile, steel, stainless steel, and aluminum are suitable materials for drop-forged parts. The specific alloy depends on the operating conditions and the required properties. These include, for example, strength, toughness, corrosion resistance, or low mass. We will determine the material grade, required condition, and availability for your project.
No. "Quenching and tempering" refers to the process of hardening followed by tempering and is one possible heat treatment for suitable steels. Depending on the material and the desired final condition, other treatments or controlled cooling from the forging heat may be considered. The decisive factor is the properties the component must possess upon delivery.
It is not possible to specify a fixed minimum order quantity in general terms. Tooling and setup costs must be considered together with material costs, follow-up work, testing expenses, and planned demand. Richter Formteile evaluates these factors based on your drawing. The costs incurred until the product is ready for delivery are also factored into the comparison with other processes.
A redesign can be evaluated based on the drawing and the component’s function. In doing so, we consider, among other things, the material, geometry, machining allowances, and required validation. Together with you and the manufacturing partner, we determine which changes would be necessary and whether they make technical and economic sense. Prototyping then serves as a test prior to the start of series production.
It would be helpful if you could provide your drawings or existing 3D data, details about the application and annual requirements, as well as any known specifications regarding materials, tolerances, and delivery condition. Please also specify any special inspection requirements. If there are still any unresolved issues, we will work with you to determine what information is needed for technical evaluation and to prepare a reliable quote.
Your Questions About the Forging Project
Would you like to discuss a technical question first or clarify the next steps? Your contact at Richter Formteile will discuss your requirements with you and guide you through the rest of the process.
Timo Richter
Managing Director
+49 7152 90171-0
t.richter@richterformteile.com
Request a Forging Project
Send us your drawing and the requirements you already know. Richter Formteile will work with you to determine the suitability of the process, the technical implementation, and the next step toward your production part.